
Search
Additional Links Contact Us- Phone: (800) 423-4198
- Toll-Free: (815) 885-1900
- Email: [email protected]
ProMach is your partner from start to finish. Our product brands are grouped into distinct business lines that make the most sense to our customers, covering every function of the production line: Filling, Bottling & Capping, Decorative Labeling, Flexibles & Trays, Pharma, Handling & Sterilizing, Labeling & Coding, Robotics & End of Line, and Systems & Integration.
learn more


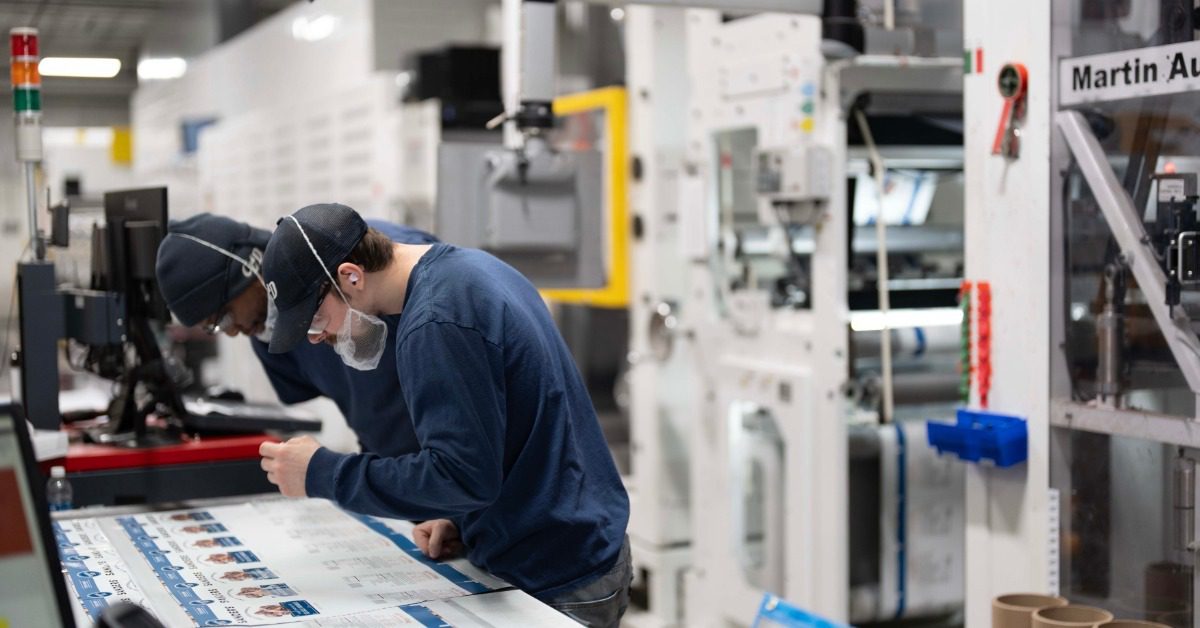
A strong pouch seal starts with the film running through your packaging line. If that material doesn't respond well to the sealing conditions, maintaining a reliable closure becomes harder throughout production. Paying close attention to film selection and seal integrity performance helps you choose materials that work with your process instead of forcing operators to compensate for a poor match. With the right film, you can build a more consistent sealing process from the start.
A seal must maintain the package closure under the conditions your product encounters, but maximum strength isn't always the only objective. Some applications may require an upper strength limit when consumers need to peel the package open.
Consider those requirements in relation to your production line. A laboratory heat-seal curve gives you useful starting data, but production equipment may produce different results because operating scale and processing speed differ from laboratory conditions. Therefore, you need to validate the material under realistic machine settings rather than relying entirely on supplier data or laboratory results.
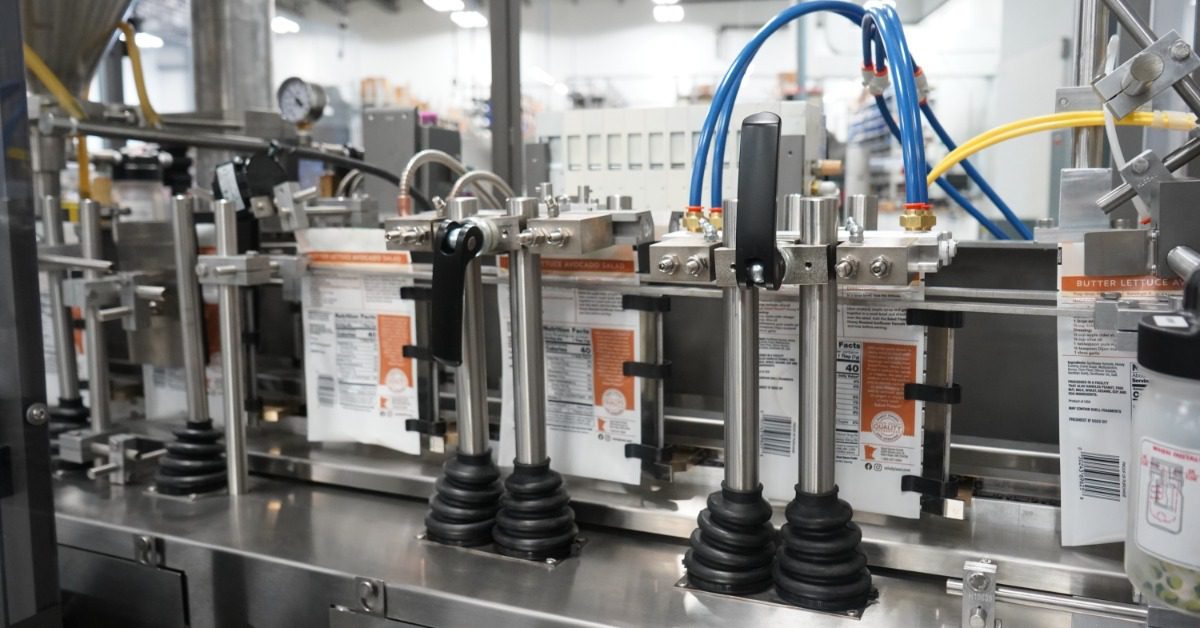
When you evaluate a multilayer film, pay close attention to the surface that forms the heat seal. Two films that look similar on a specification sheet may respond differently once they reach the sealing jaws.
You should evaluate the sealant layer as part of the complete package structure. During material trials, film selection and seal integrity performance depend on whether the entire film construction works under your actual production conditions. Testing the complete structure helps you determine if the film is a reliable fit for your packaging line.
You need to consider total web thickness because heat must travel through the material before the sealing surfaces reach the conditions needed for bonding. Web construction and total thickness affect sealing properties, especially when short dwell times limit heat transfer. Consequently, material thickness deserves attention alongside the properties of the sealant layer.
Key questions can help guide your material review:
Film performance doesn't exist in isolation. Seal integrity is influenced by the interaction between film construction, package design, machine capabilities, and operating conditions. Evaluating those factors together often produces better results than focusing on any single variable.
As part of ProMach's Flexible Packaging Group (FPG), HMC collaborates with CL&D and other flexible packaging specialists to help manufacturers take a more comprehensive approach to packaging decisions. By bringing together expertise in packaging machinery, film graphics, and package performance, the group helps customers evaluate how materials and equipment work together under real production conditions. That broader perspective can help identify compatibility issues earlier, streamline material qualification, and support more reliable sealing performance across the packaging line.
Your film and packaging equipment need to work as one production system. FFS machine manufacturers develop equipment that must accommodate specific film properties, making material compatibility an important factor in establishing reliable sealing parameters and production speeds.
Before changing materials, you should review what the new structure requires from the sealing process. A film that needs different heat-transfer conditions may require you to revisit established settings rather than loading the roll and expecting the previous recipe to work. Production trials help you identify those differences before a full run.
As you increase production speed, you generally reduce the time available for individual sealing operations. Short dwell times may prevent the sealing interface from reaching jaw temperature. Under those conditions, the full web construction influences the resulting seal strength. Therefore, a film that performs well at one rate deserves another evaluation at a faster rate.
You need enough heat at the sealing interface to create the intended bond, but the jaw temperature alone doesn't describe what the film experiences. Heat must transfer through the web, and construction differences affect that transfer. This distinction helps explain why simply copying a temperature setting from another material may produce inconsistent results.
When you introduce a different film, establish settings through controlled trials. Adjust conditions based on measured seal results. That process gives you a clearer picture of the usable sealing range before routine production begins.
A seal's job doesn't end when the jaws release the pouch. You need to consider the forces a package may encounter as it moves through subsequent handling and distribution. Seal-strength testing measures closure performance, while other methods address different aspects of package integrity.
Because these tests answer different questions, you shouldn't treat one successful measurement as proof of every aspect of seal performance. ASTM F2029, for example, focuses on heat sealing as measured by seal strength and specifically excludes continuity measurements such as air-leak or dye-penetration testing. Choose evaluation methods that correspond with the risks you need to understand.
A controlled trial gives you an opportunity to see what the film does on your equipment. You can compare seal results against your acceptance criteria while watching for variation as the line runs. Additionally, a trial helps separate a promising laboratory result from material performance under real production conditions.
Build the trial around measurable observations by:
Changing film suppliers or film structures requires careful evaluation because sealing performance depends on the material running through the machine. Changes in film thickness or sealant composition can affect heat transfer and the conditions needed to create a reliable seal. As a result, you should validate new films under actual production conditions and adjust sealing parameters when necessary.
Keep useful records from each material qualification so you have a reference when performance changes later. If a seal problem appears after a material change, documented trial conditions give your team somewhere concrete to begin investigating. That history also helps you distinguish material-related variation from equipment adjustments.
Choosing film that matches your packaging process gives operators a dependable range of settings for maintaining seal quality. Validating the material under actual production conditions confirms that its construction works with the equipment rather than forcing operators to compensate through repeated adjustments. With that compatibility established, you can maintain more consistent seal performance throughout production.
HMC Products supports horizontal pouch packaging operations with new HMC Pouchmasters as well as rebuild, consulting, and training services. If you're evaluating a film change or trying to improve sealing consistency on an HFFS line, speak with us about the equipment conditions that should factor into your next material trial.